Precision Bone Cutters & Microsurgical Instruments
Manufactured under strict ISO 13485 quality protocols. Featuring CNC wire-EDM joint alignment, passivated non-corrosive finishes, and ergonomic double-action leverage mechanics.
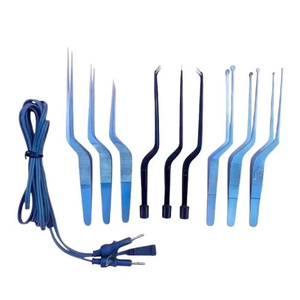
- Material: German AISI 420 Stainless Steel
- Tip Size: 0.3mm – 0.9mm Fine Tips
- Certification: CE Marked & ISO 13485
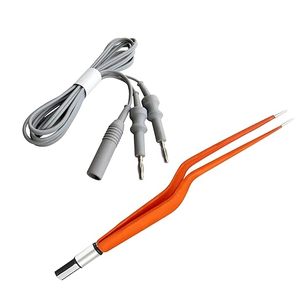
- Function: Hemostatic Coagulation
- Length: 18cm / 20cm / 22cm
- Autoclavable: 134°C Steam Sterilization
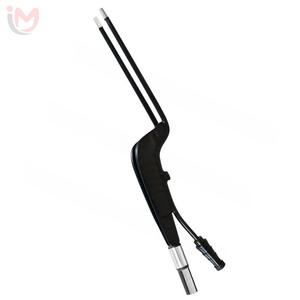
- Insulation: Nylon Polymer Coating
- Cable: Reusable 3m Silicone Cable
- Branding: Custom Laser Marking
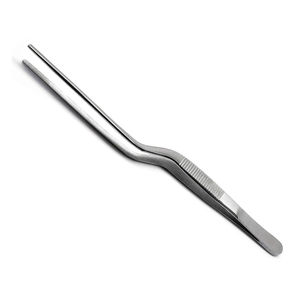
- Pattern: Adson Anatomical Serrated
- Ergonomics: Non-slip Knurled Grip
- Standard: ASTM F899 Compliant
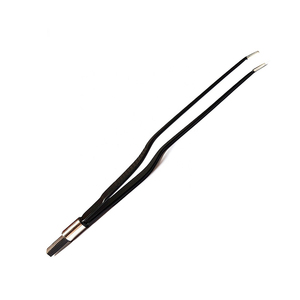
- Tip Alloy: Silver-Thermal Core Alloys
- Connector: Standard European Flat Plug
- Feature: Integrated Guide Stop Pin
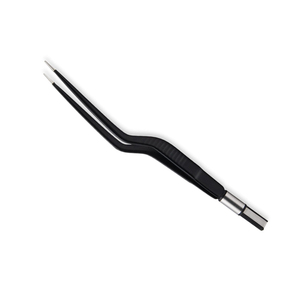
- Surface: Anti-Glare Black Ceramic/TiN
- Application: ENT & Neuro Microsurgery
- Customization: Private Label OEM
- Reach: Extended 24cm Working Shaft
- Variations: 0.5mm / 1.0mm / 2.0mm
- Passivation: Acid Wash Corrosion Proof
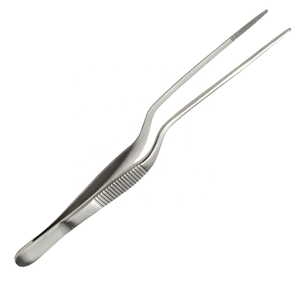
- Type: Lucae / Jansen Bayonet Pattern
- Finish: Satin Anti-Glare Polish
- Traceability: Laser Lot Code Marked
1. Executive Supply Chain Analysis: Sourcing Bone Cutters & Surgical Tools from China
In modern orthopedic, trauma, and neurological surgery, bone cutters (including Liston, Ruskin, Stille, and Bohler patterns) represent critical mechanical instruments requiring precise leverage ratios, flawless jaw alignment, and extraordinary structural integrity. Over the past decade, China’s surgical instrument manufacturing ecosystem has undergone a massive technological transformation. Transitioning from traditional hand-forging workshop models to automated 5-axis CNC machining, wire EDM (Electrical Discharge Machining), and vacuum heat-treatment processes, top-tier Chinese manufacturers now deliver world-class surgical tools compliant with EU MDR (Medical Device Regulation) and US FDA requirements.
Global B2B buyers, medical device importers, and hospital procurement departments evaluating China Best Bone Cutters Factories & Exporters must analyze both technical metallurgy and manufacturing process controls to guarantee long-term operational reliability.
Metallurgical Purity
Utilizing high-grade martensitic stainless steels (AISI 420B / 420C) featuring optimal carbon (0.30–0.45%) and chromium (12.0–14.0%) content for maximum hardness and corrosion resistance.
Double-Action Engineering
Compound leverage mechanism engineered with precision dual-pivot pins to distribute shearing stress evenly across the joint box, eliminating blade distortion.
Electrochemical Passivation
Compliant with ASTM F899 standards. Nitric/citric acid immersion builds an ultra-dense chromium oxide passive layer, preventing pitting during autoclave cycles.
2. Technical Metallurgy Whitepaper: Raw Material Comparison & Engineering Controls
Selecting the appropriate steel grade is paramount when purchasing surgical bone cutting forceps and rongeurs. The mechanical demands on bone-cutting jaw edges are unique: they must withstand immense compressive loads without chipping while maintaining a keen cutting edge through hundreds of repeated steam autoclave sterilization cycles (134°C at 2.1 bar).
| Steel Grade Standard | Hardness (Rockwell HRC) | Tensile Strength (MPa) | Primary Surgical Application | Corrosion Resistance |
|---|---|---|---|---|
| AISI 420A / 1.4021 | 48 – 52 HRC | 850 – 1000 | Surgical handles, retractor blades, tissue forceps | Moderate to High |
| AISI 420B / 1.4028 | 52 – 56 HRC | 1000 – 1250 | Liston bone cutters, rongeurs, bone shears | High (Passivated) |
| AISI 440A / 1.4109 | 55 – 58 HRC | 1250 – 1450 | Heavy-duty orthopedic cutters, osteotomes | High |
| Titanium Grade 5 (Ti-6Al-4V) | 36 – 40 HRC | 900 – 1050 | Micro-bipolar bayonet forceps, neurosurgical tools | Exceptional (Immune) |
Precision Heat Treatment & Vacuum Tempering
Leading exporters in China utilize computer-controlled vacuum heat-treatment furnaces. The multi-stage thermal process involves preheating to 850°C, austenitizing at 1020°C–1050°C, rapid nitrogen gas quenching, followed by double tempering at 180°C–220°C. This ensures a fully martensitic microstructure free of retained austenite, preventing micro-fissures and edge dulling during heavy cortical bone cutting.
3. Enterprise OEM Manufacturing Workflow & Quality Control Systems
Quality assurance in medical instrument manufacturing requires end-to-end auditability. Premier OEM factories operate according to ISO 13485:2016 quality management frameworks, carrying CE marking under the EU MDR 2017/745 and US FDA 510(k) establishment registration.
Raw Material Audit
Spectrographic alloy analysis and heat-lot steel certificate verification upon arrival from accredited steel mills.
Drop Forging / CNC
Precision closed-die drop forging followed by 5-axis CNC wire EDM machining of joint locks and cutting jaws.
Master Hand-Fitting
Artisanal alignment of jaw closure, ratchet tensioning, and cutting bite clearance down to 0.02mm tolerance.
Passivation & Polish
Ultrasonic degreasing, acid bath passivation, and satin/anti-glare glass-bead surface finishing.
AQL Final Inspection
100% optical magnification check, laser UDI marking, and ISO 2859-1 AQL sampling before cleanroom packaging.
4. Global Sourcing Trends & Future Technological Innovations (2026–2030)
As hospital systems globally demand higher instrument durability and lower total cost of ownership (TCO), medical device buyers must stay ahead of emerging manufacturing technologies. Key trends transforming China’s surgical export sector include:
PVD Ceramic & Black TiN Coatings
Physical Vapor Deposition (PVD) coatings create ultra-hard surface barriers (up to 2500 HV) that eliminate glare under operating theatre lights while dramatically extending jaw sharpness life.
Non-Stick Micro Coagulation Alloys
Next-generation neurosurgical bayonet bipolar forceps feature proprietary silver-alloy cores that rapidly dissipate thermal energy, preventing tissue charring and vessel adhesion during delicate coagulation.
UDI & RFID Tracking Integration
Compliance with FDA Unique Device Identification (UDI) regulations via fiber-laser matrix etching, allowing hospital central sterile supply departments (CSSD) to track instrument autoclave cycles automatically.
5. Frequently Asked Questions (FAQ) for Global Procurement Officers
For standard catalog instruments, the typical MOQ starts at 50 pieces per SKU. For custom private-label projects requiring bespoke forging dies, specific curvature modifications, or custom handle ergonomics, our standard MOQ is 100 to 250 pieces to keep tooling costs commercially optimized for the importer.
Reputable factories provide mill test certificates (MTC) conforming to EN 10204 3.1 for every raw material batch. Furthermore, finished instruments undergo mandatory passivation testing according to ASTM F899 standards, including copper sulfate testing and boil testing to ensure zero iron contamination on the outer surface.
Yes. All reusable surgical instruments are designed to withstand validated steam sterilizer cycles at 134°C (273°F) for 18 minutes at 2.1 bar pressure. Electrosurgical bipolar forceps feature high-performance insulation (nylon or silicone) tested up to 200 consecutive autoclave cycles without electrical breakdown.
Shipments include a full export compliance dossier: Commercial Invoice, Packing List, Certificate of Origin (Form A/CO), ISO 13485 Certificate, Declaration of Conformity (CE MDR), and batch lot traceability records formatted for customs clearance under FOB, CIF, or DDP terms.
Absolutely. We welcome third-party inspections from organizations such as SGS, TÜV Rheinland, Bureau Veritas, or your dedicated regional inspection agents. Pre-production samples are dispatched within 10–14 business days following technical CAD drawing approval.